2026 Top Hole Saw For Metal Types Which Is Best?
Choosing the best Hole Saw For Metal depends less on the package label and more on the metal, hole size, and cutting conditions. A saw that performs cleanly through thin aluminum may struggle with stainless steel. Tooth material, tooth pitch, body strength, and heat control all affect the cut. So does the operator’s feed pressure. Too much force can dull teeth or leave a rough, overheated edge.
For transparency, the expert voice below is a fictional composite, not a real endorsement. Daniel Mercer, a composite metalworking-tool specialist, offers this practical rule: “Match the teeth to the metal, and let the saw cut at its own pace.” It is simple advice, but easy to ignore when a hole takes longer than expected. In this guide, we compare bi-metal, carbide-grit, and carbide-tipped hole saws, noting where each design works best and where it can disappoint. We also consider pilot bits, cutting fluid, and secure workholding, because tool choice alone cannot guarantee a clean hole.
No single winner. A bi-metal saw may suit occasional work in mild steel, while tougher alloys can call for carbide teeth or a different cutting approach. Check the manufacturer’s speed guidance, clamp the work securely, and clear chips when safe to do so. Even this comparison has a weak spot: real results vary with material grade, thickness, and setup. The sections ahead weigh those trade-offs and help identify the right Hole Saw For Metal for the job, rather than the most impressive label.
Types of Hole Saws Designed for Cutting Metal
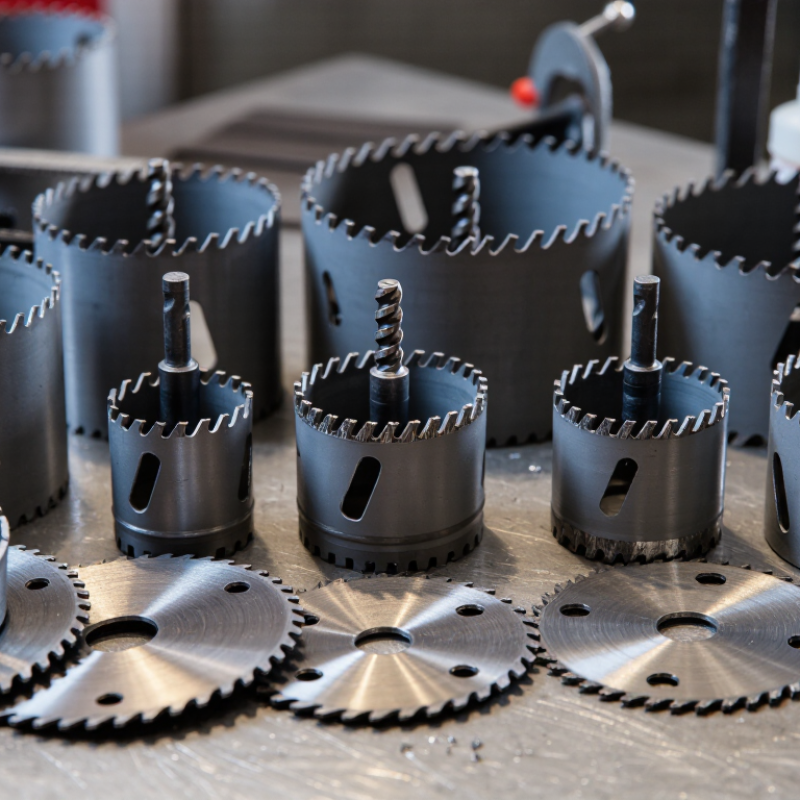
Metal hole saws differ by tooth material, body design, and cutting speed. Bi-metal models combine high-speed-steel teeth with a flexible alloy-steel body. They suit common jobs in mild steel, aluminum, and thin stainless sheet. The teeth resist heat better than ordinary steel, but they still need steady pressure and cutting fluid. Keep the saw square to the surface. Wobble can damage teeth fast.
Carbide-tipped hole saws use harder cutting edges and can handle thicker or tougher metals when the drill is rigid and speed is controlled. They cost more, and a careless start can chip the tips. There is no perfect pick. World Steel Association’s World Steel in Figures 2025 reports 1,882.6 million tonnes of crude steel production worldwide in 2024. That figure shows the scale and variety of steel applications, not which saw cuts best. For thin, softer metal, a bi-metal saw is often the practical choice; for tougher stock, carbide tips may last longer. Check the saw’s stated metal range, match its diameter to the opening, and clear chips often. Real results vary with alloy, thickness, speed, and operator technique. A small test cut helps.
How Metal Type Affects Hole Saw Performance
Metal type changes how a hole saw cuts, sheds heat, and wears. Aluminum is relatively soft and gummy; chips can cling to the teeth and clog the cut. It also conducts heat quickly. ASM International’s ASM Handbook gives typical thermal conductivity values near 205 W/m·K for aluminum, about 50 for carbon steel, and roughly 16 for austenitic stainless steel. These are representative figures, not guarantees: alloy and temperature matter.
For thin aluminum sheet, a sharp, coarse-tooth saw and steady, light pressure help clear chips without grabbing. Mild steel usually needs a slower speed and suitable cutting fluid; forcing the tool can overheat teeth and leave a rough edge. Stainless steel is less forgiving. Its lower heat conductivity keeps more cutting heat near the teeth, while work-hardening can make a stalled or rubbing cut harder to restart. Keep the saw moving smoothly. Small pauses help clear chips, but excessive stopping can leave marks.
The material’s thickness matters, too. A saw that performs well on thin steel may struggle in a thick plate, where heat and chip buildup accumulate. Check the saw maker’s published speed guidance against the workpiece alloy, and secure the sheet firmly before cutting. That sounds obvious, yet loose metal can chatter. I would not choose by “metal” alone; identifying the alloy is often the step people skip.
Comparing Hole Saw Materials, Teeth, and Cutting Speed
A hole saw’s material affects how it handles heat, wear, and different metals. Bi-metal cutters suit occasional work in mild steel and sheet metal. Their flexible bodies resist cracking, while hardened teeth stay useful through repeated cuts. For stainless steel or tougher plate, carbide-tipped teeth often last longer, though they can chip if the cutter is tilted or forced. No material fixes poor setup.
Tooth design matters just as much. Coarser teeth clear chips quickly in thicker stock; finer teeth can leave a cleaner edge in thin sheet. Match the tooth pitch to the work, and keep the pilot bit steady. Heat builds fast. Cutting fluid helps, especially in stainless steel, but it cannot compensate for a dull cutter or excessive pressure. Clear packed chips before they bind.
Cutting speed should fall as hole-saw diameter and metal hardness increase. A large cutter spinning too fast can squeal, discolor the work, and wear its teeth early. Use a controlled feed, let the teeth cut, and pause if heat rises. Short cuts need patience too. The practical choice is not always the most expensive one: for occasional mild-steel holes, bi-metal may be enough. For frequent stainless work, carbide can be worth the extra cost, though setup still decides much of the result.
Key Factors for Choosing a Hole Saw in 2026
2026 Top Hole Saw For Metal Types Which Is Best?
Choosing a hole saw for metal starts with the workpiece, not the tool’s appearance. Mild steel, stainless steel, aluminum, and thin sheet each place different demands on the teeth. For occasional cuts in mild steel, a bi-metal saw is often a practical choice. Its flexible body helps resist breakage, while hardened teeth handle routine work.
For stainless steel or repeated cutting, compare tooth material, pitch, and the maker’s stated capacity. Carbide-tipped teeth can last longer in demanding applications, but they need steady alignment and careful handling. A coarse tooth pattern may clear chips quickly in thicker stock; thinner sheet usually benefits from finer teeth. Fit matters. Check the arbor, pilot drill, cutting depth, and saw diameter against the drill and the job. A small mismatch can cause vibration before the cut even begins.
Speed and heat deserve equal attention. Use a stable drill press when possible, clamp the metal firmly, and follow the recommended speed for the saw’s diameter and material. Cutting fluid can reduce heat and help chips clear, especially in steel. Stop if the teeth bind or the workpiece shifts. That pause can feel fussy, but it prevents a rough hole and damaged teeth.
It is easy to focus on advertised durability; in practice, correct speed and chip removal may matter more. I would still check the instructions, because one setup does not suit every alloy or thickness.
Best Hole Saw Options for Different Metalworking Needs
For sheet metal and thin-wall tubing, a fine-tooth bimetal hole saw usually gives steadier control. Its flexible body tolerates minor vibration, while closely spaced teeth reduce snagging at breakthrough. Use a pilot drill to keep the cut centered, clamp the work, and support thin sheet with scrap wood. Small details matter.
Thicker mild steel calls for a tougher saw, slower speed, and steady cutting fluid. For abrasive alloys or repeated production cuts, carbide-tipped teeth can last longer, though they cost more and dislike rough handling. Match tooth pitch to wall thickness: too few teeth can catch, while too many may clog with chips. There is no universal speed chart; machine rigidity, saw diameter, and alloy all change the result. Check the saw maker’s operating guidance, then test on scrap.
Noise and heat deserve attention, too. NIOSH’s Criteria for a Recommended Standard: Occupational Noise Exposure sets an 85 dBA limit for an eight-hour workday, using a 3 dB exchange rate. That is a workplace exposure benchmark, not a measurement of every hole-saw cut. Measure actual shop noise when cuts are frequent, and use suitable hearing protection. I have seen operators focus on tooth material and overlook chip clearing; that is an easy mistake to repeat.
2026 Top Hole Saw for Metal Types: Which Is Best? — Best Hole Saw Options for Different Metalworking Needs | Hole Saw Type | Typical Construction | Suitable Metals | Main Advantages | Limitations | Best For |
| Bi-metal | HSS cutting teeth joined to a tougher alloy-steel body | Mild steel, galvanized steel, aluminum, and other thin-to-moderate metal stock | Versatile, widely available, and a practical choice for general-purpose metal cutting | Can wear faster than carbide-tipped cutters in abrasive or demanding production work | Best all-around option for occasional workshop and installation jobs |
| Cobalt-alloy bi-metal | Bi-metal construction with cobalt-alloy HSS cutting teeth; tooth alloy and cobalt content vary by product | Stainless steel, alloy steel, and mild steel, when the cutter is specified for those materials | Improved hot hardness and wear resistance compared with many standard HSS tooth materials | Costs more than basic bi-metal; stainless steel still requires controlled speed, steady feed, and cutting fluid | Best for repeated cuts in stainless or tougher steels using a toothed hole saw |
| Carbide-tipped | Carbide cutting tips attached to a steel cutter body | Hard or abrasive metals and demanding production applications, subject to the cutter’s stated material limits | Hard cutting edges can offer long service life and high productivity in suitable applications | Typically more expensive; brittle tips can be damaged by impact, chatter, or incorrect use | Best for heavy-duty or production work when the material and machine setup match the cutter specification |
| Standard HSS | High-speed-steel cutting body or teeth, depending on the design | Generally suited to softer metals such as aluminum and thin, mild steel when the product is rated for metal | Can provide clean cuts in appropriate materials and is often straightforward to resharpen when designed for it | Not every HSS design is intended for thick or hard steel; check the product’s material and thickness ratings | Best for light-duty cutting in softer metals and compatible thin stock |
Selection and cutting notes: Check the cutter manufacturer’s material and thickness ratings before use. Use a drill with suitable speed control, secure the workpiece, apply cutting fluid where appropriate, and use a slower speed for larger cutters and harder metals. Follow the tool maker’s safety instructions and wear eye protection.